

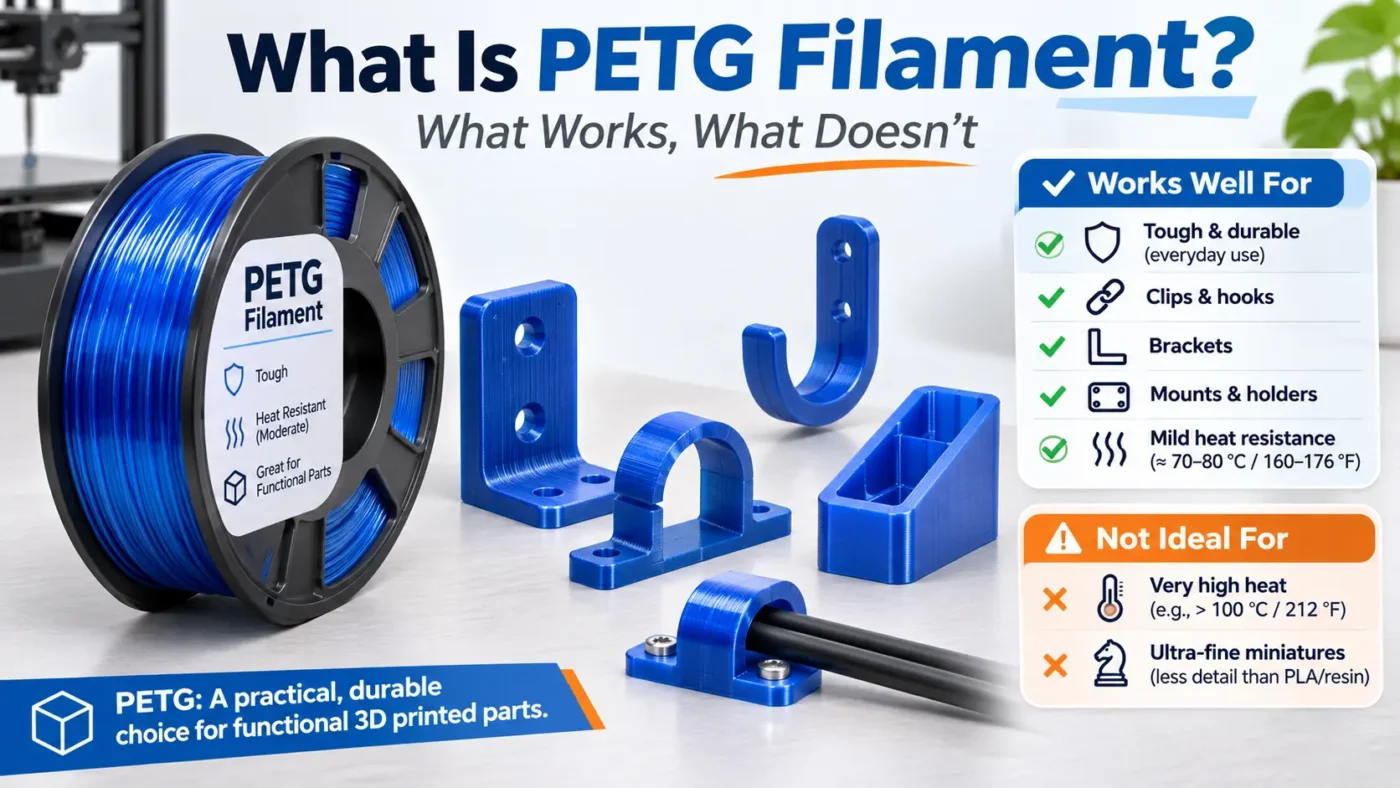
PETG filament is a polyester filament for FDM 3D printers — tougher and more heat-resistant than PLA filament, easier to print than ABS filament.
Its full name is polyethylene terephthalate glycol-modified: the “glycol-modified” part is what stops the material from crystallizing, so it prints at moderate temperatures instead of needing industrial equipment.
If you want the one-line verdict: print PETG when the part has to survive a drop, a clip-in fit, or warm surroundings; print PLA when you want clean detail and stiffness.
The 30-second selection guide
Read the left column. Print the right column.
| If your part needs to… | Use |
| Look sharp, hold fine detail, or stay indoors as a display piece | PLA |
| Flex instead of crack, survive drops, clip onto something, or work in mild heat | PETG |
| Sit in a hot environment — direct sun in summer, near a heater, under a hood | ASA / ABS (not PETG) |
| Stretch, bend, or grip like rubber | TPU |
| Touch food directly | Nothing printed on an FDM printer (see the myths section) |
That is the whole decision for most people. Everything below explains why.
What PETG is actually good at — and where it stops
| Works well | Has limits |
| Toughness. Bends under load instead of shattering, so clips and brackets survive. | Not a high-temperature engineering plastic. Keep parts below roughly 60–70 °C in use. |
| Heat resistance above PLA. A printed part left in a warm car holds up better than PLA. | Still deforms well before ABS/ASA territory. |
| Layer bonding. Layers weld together well, so parts resist splitting along layer lines. | Good bonding also means supports fuse on. Support scars are common. |
| Low warping. Big flat parts usually print on an open-frame printer. | Not warp-free. Long, thin, or sharp-cornered parts still lift without a brim. |
| Glossy surface. Clean, slightly shiny skin; translucent and clear-tinted versions exist. | Translucent does not mean glass-clear. Expect a frosted, visible-layer-line look. |
| Stringing control. Once dialed in, prints come out clean. | Fresh out of the box it strings and oozes more than PLA. |
PETG vs PLA vs ABS
| PETG | PLA | ABS | |
| Toughness (resists breaking) | Low — snaps | High | Medium-high |
| Rigidity (resists bending) | High | Medium | Medium |
| Heat resistance | Low | Medium | High |
| Warping | Low | Low-medium | High |
| Fumes / smell | Low | Low | Noticeable, needs ventilation |
| Enclosure needed | No | No | Usually yes |
| Surface | Matte to satin | Glossy | Satin, can be smoothed with vapor |
| Typical use | Models, prototypes, decor | Functional parts, jigs, clips, cases | Hot or mechanically stressed parts |
Three things people get wrong when reading a table like this:
1. Rigid is not the same as tough. PLA is stiffer — it resists bending — but that stiffness is why it snaps. PETG gives a little, then springs back.
2. “Stronger” needs a definition. Load capacity depends on the formulation, print orientation, layer bonding, and part design. No filament wins every test.
3. There is no best filament, only a best match. PETG’s balance of toughness, heat resistance, and printability is why it is the default for everyday functional parts.
Real parts: what PETG is used for
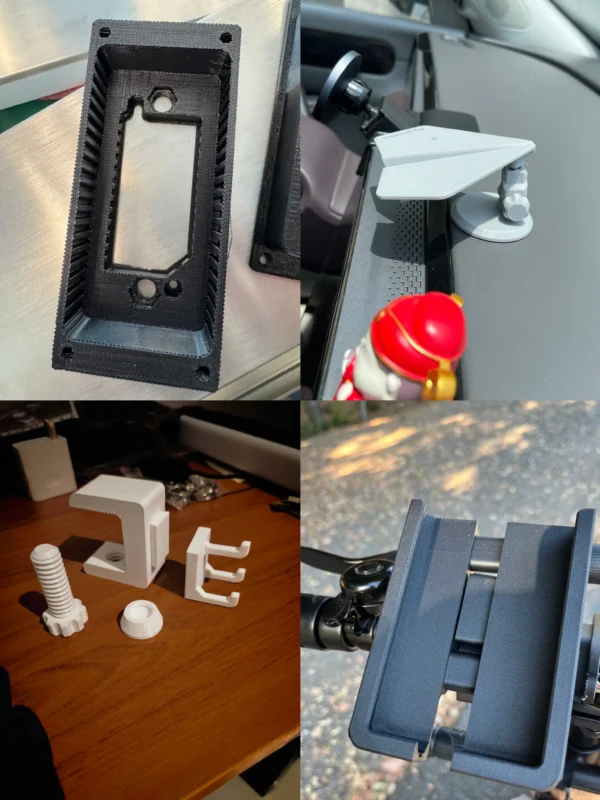
– Clips, hooks, and cable guides — flex to snap on, then stay put.
– Brackets, mounts, and jigs — tolerate tightening torque without cracking.
– Tool holders and workshop fixtures — survive being dropped on concrete.
– Replacement knobs, latches, and handles — warm to the touch in use, no sag.
– Enclosures, boxes, and trays — large flat geometry, low warping.
– Phone stands, tablet holders, headphone hooks — light load, long service life.
– Drone frames, RC parts, camera mounts — impact resistance beats stiffness.
– Garden stakes and outdoor-ish parts — with the caveat that PETG is only moderately UV-stable; long-term sun exposure still degrades it.
– Plant pots and vases with a waterproof liner — PETG is not watertight by itself at typical layer heights.
If the part is going to be looked at closely and never stressed, PLA is the cheaper, sharper choice.
What PETG is not good for
Skip PETG for these jobs:
– Hot service. Engine-bay parts, dishwasher-safe items, anything near a heater or in direct summer sun under load. It will creep and distort.
– Fine miniatures and high-detail display models. Ooze and stringing soften edges that PLA holds crisply.
– Complex support structures. PETG fuses to its own supports; removal leaves scars. Design to avoid supports, or use a dedicated support material.
– Glass-like transparency. Thin walls with visible layers are the realistic result.
– Food-contact and medical use. Layer gaps trap residue. See below.
– Parts that need maximum stiffness per gram. PLA, or a filled/engineering material, is stiffer.
– Long bridges and steep overhangs on a stock profile. It can be done, but it needs part cooling and slower speeds than PLA.
PETG Print Settings & Tips
Getting the right PETG print settings can improve layer adhesion, reduce stringing, and achieve smoother results. Proper filament drying is also important for consistent print quality.
For recommended temperatures, print speeds, cooling, retraction, drying methods, and troubleshooting tips, explore our Complete PETG Printing Guide.
Food contact and safety: five myths
– “PETG is food-safe, so a printed cup is safe.” The base resin may be food-contact rated; the printed part is not. Layer lines create gaps that hold residue and bacteria. No printed part should be treated as food-safe without a coating and testing.
– “No smell means no emissions.” PETG is low-odor, not emission-free. Print with airflow, as you would with any filament.
– “BPA-free means safe for kids.” BPA-free is a materials statement, not a product-safety statement. Small printed parts are still choking hazards. If the household project involves a child’s 3D pen, read [are 3D printing pens safe for kids]and the [3D pen age buying guide].
– “PETG is stronger than PLA, full stop.” It is tougher and more heat-resistant. PLA is stiffer. Different jobs.
– “PETG doesn’t need drying.” It is more hygroscopic than PLA. This is the single most common cause of “bad batch” complaints.
Printer compatibility
– Open-frame printer: fine.This is PETG’s main practical advantage over ABS.
– Enclosure: not required.Helpful for very large parts and drafts, not mandatory.
– Hotend: a standard PTFE-lined hotend handles the 220–240 °C range. If you routinely print at the top of the range, an all-metal hotend is the safer choice.
– Extruder:direct drive is easier to tune. Bowden works — expect lower retraction values than the reference settings.
– Bed surface:PEI, glass, or textured sheet, all with a release layer.
– Nozzle: brass is fine. Abrasive or filled variants need a hardened nozzle.
– Filament tolerance matters more than usual.±0.02 mm diameter keeps flow consistent; loose tolerances cause inconsistent extrusion that gets blamed on settings.
Before you buy: five checks
1. Diameter and tolerance— 1.75 mm ±0.02 mm, stated on the label.
2. Spool length or net weight — compare cost per meter, not per spool.
3. Whether it was dried and vacuum-sealed*— moisture is the most common defect.
4. Batch consistency— if you print the same part repeatedly, order from the same batch
Looking for Reliable PETG Filament?
Explore Sundi3D PETG 3D Printing Filament, available in 1.75 mm diameter for compatible 3D printing applications.
Retail orders through our online store. Shops, schools, and resellers are welcome to contact us for wholesale pricing.
